Production
The whole chain under one roof
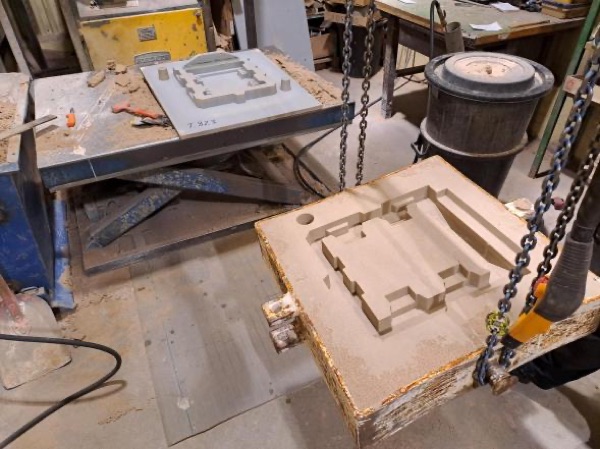
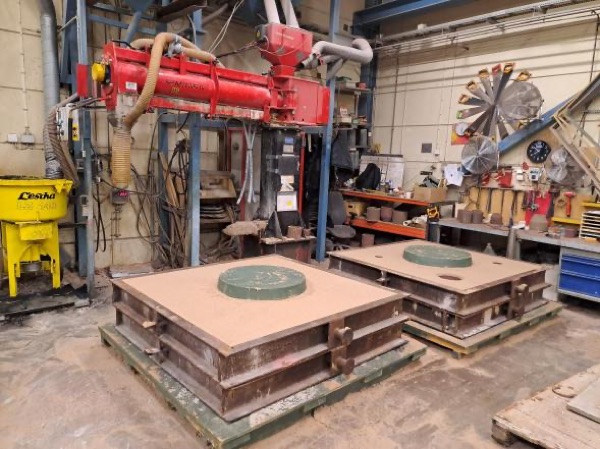
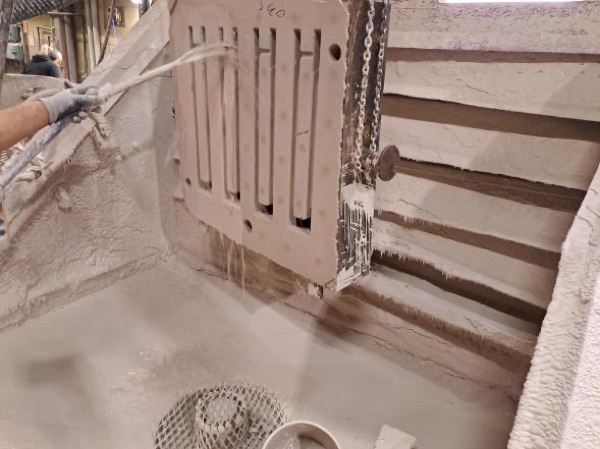
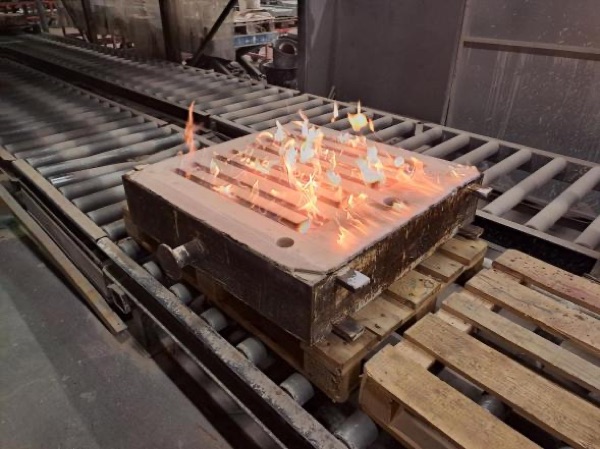
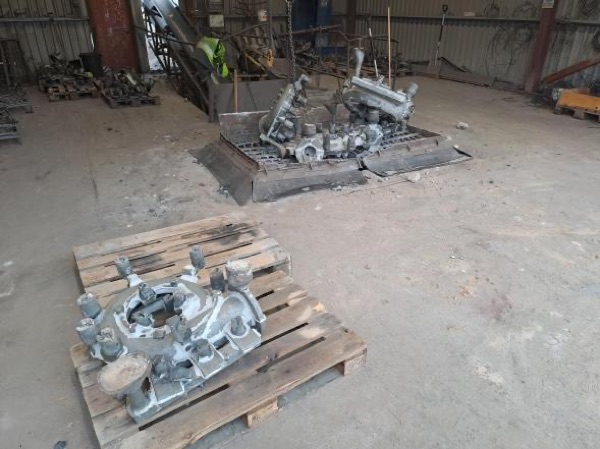
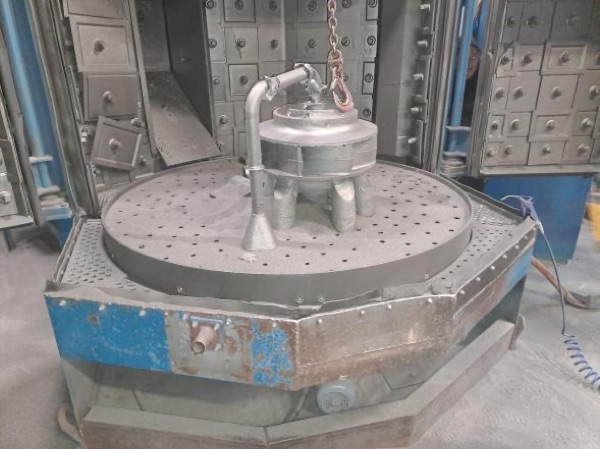
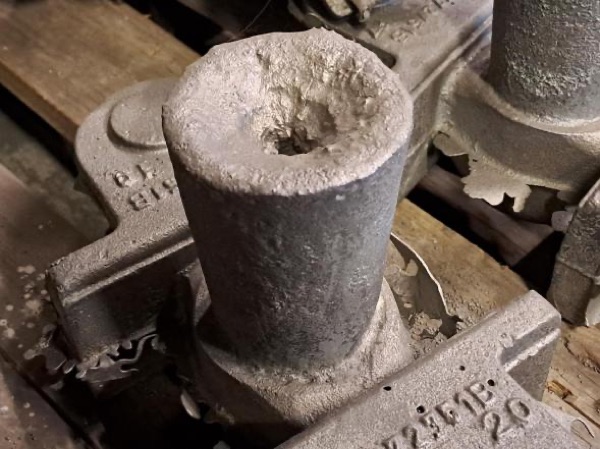
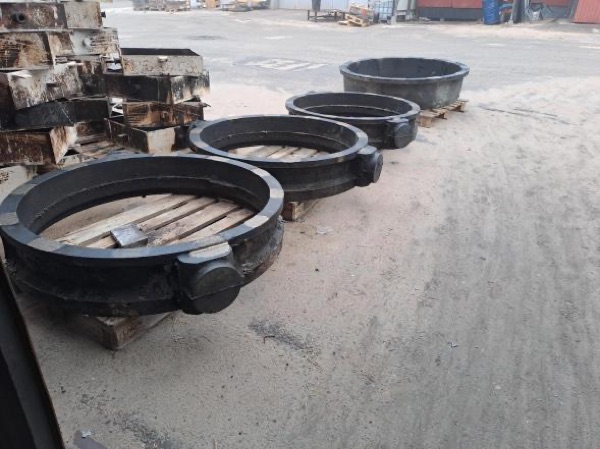
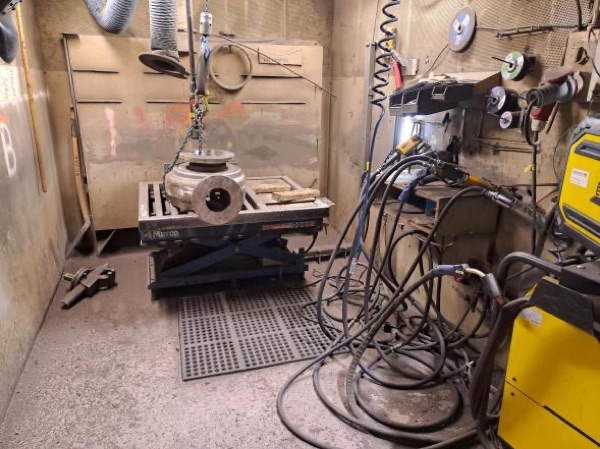
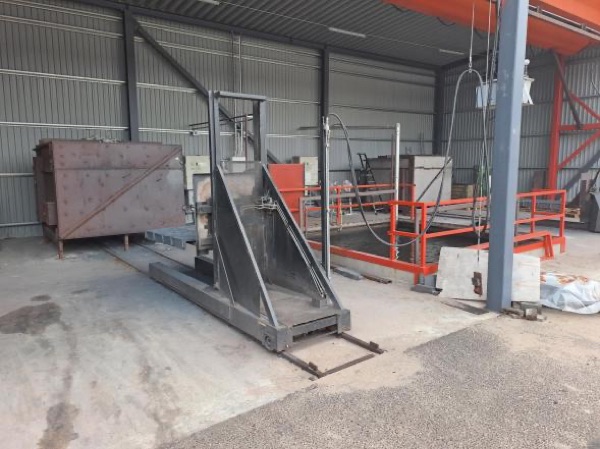
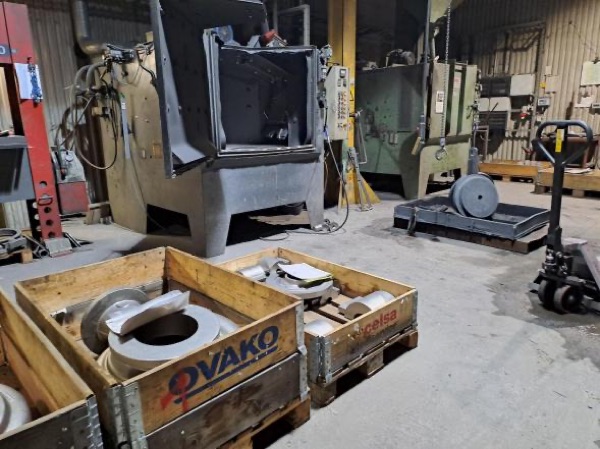
A picture series showing the foundry workflow, from pattern and mould making through to pouring the finished casting.
Gravity casting in single-use sand moulds
We cast stainless steel by gravity. The moulds are single-use sand moulds: every part gets a new mould, which is broken apart to release the casting. It sounds simple, but some twenty separate operations sit between the pattern and the inspected casting, and all of them have to be right.
This page follows the workflow step by step, with photographs from our own shop floor. A glossary of foundry terms sits at the end.
Moulding
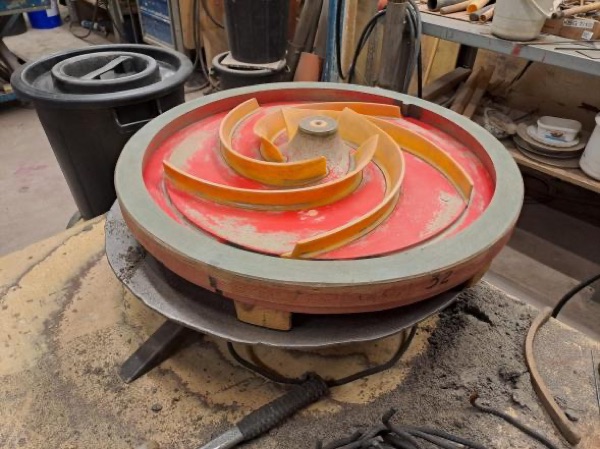
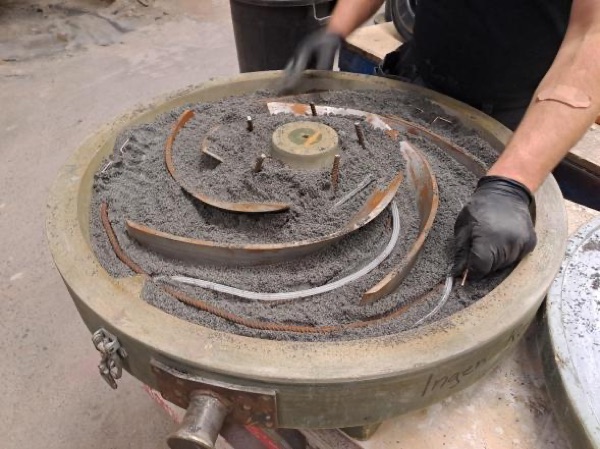
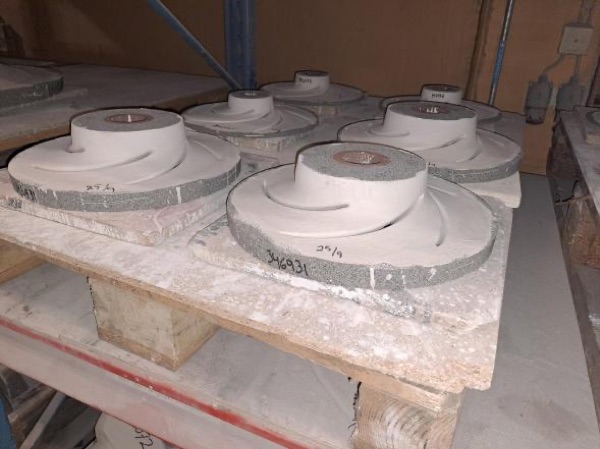
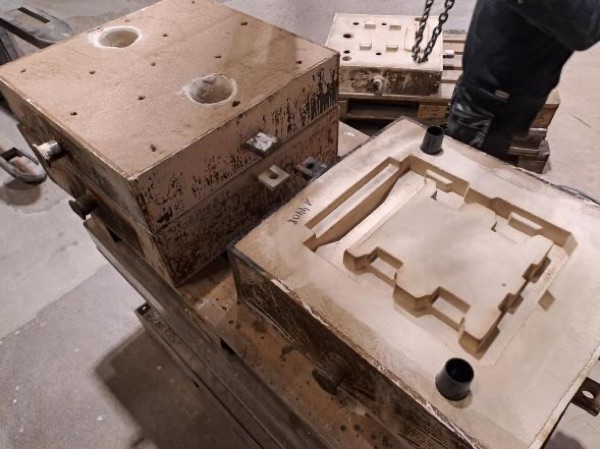
It all starts with the pattern and the core box. The pattern forms the outside of the casting, the core its inside. Moulds are made by the CO₂ method, which gives good dimensional accuracy, fine surfaces and low finishing costs.
New sand as moulding material, usually combined with zircon sand next to the pattern, contributes to the surface finish and minimises the risk of sand burning onto the casting. The coating has to be dry before the mould halves are assembled.
Casting
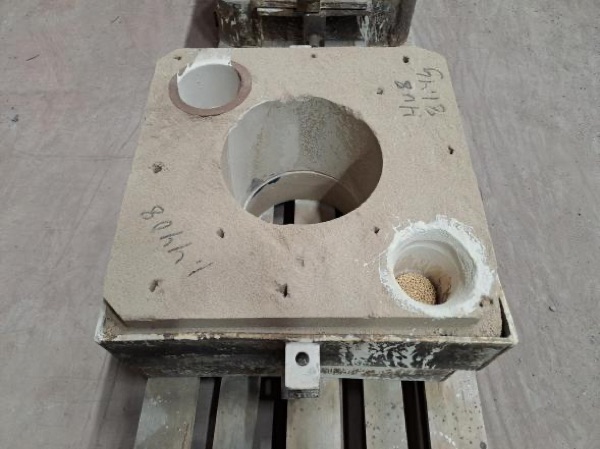
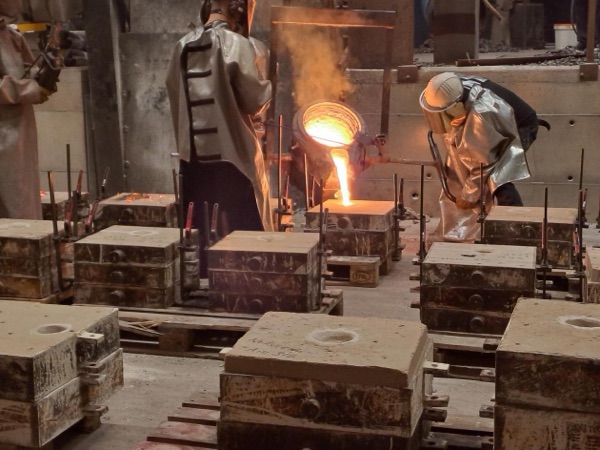
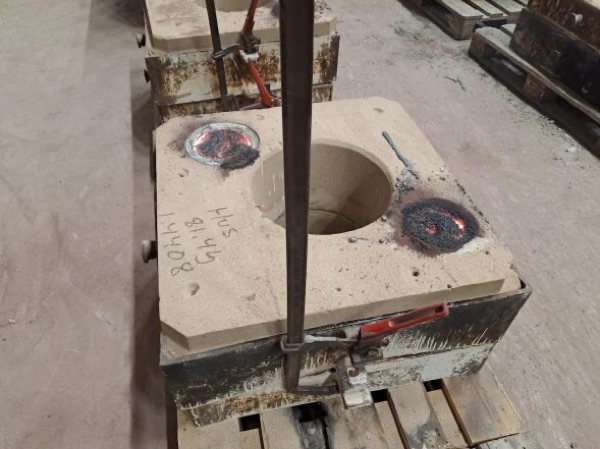
Once the mould is closed it is poured. The metal should enter low and full, without air or slag. The gating system of sprue, runner and ingate keeps the flow laminar, and the feeders compensate for the 10 % the steel shrinks as it solidifies.
We cast practically every commonly used castable steel grade, with stainless and acid-proof castings as our speciality.
Finishing
Contraction on cooling breaks up the moulding sand, and the castings are knocked out and blasted. The gating system and feeders are then cut away, and the castings are deburred and repaired in the fettling booth.
After that the castings are heat treated in a modern furnace fitted with a recorder, so the process can be followed and verified throughout. Before delivery they are blasted with a stainless medium, to remove scale and minimise the risk of discolouration. Inspection comes last.
Foundry terms
A glossary for anyone curious about the world of the foundry.
International Atlas of Casting Defects is a reference work for classifying casting defects and finding solutions to them. Designations such as B200, B111, C221 and C211 below refer to sections in that book.
SHRINKAGE
- Contraction on cooling
- If the pattern is one metre long, the finished casting comes out 2 % smaller, that is 98 cm. Patterns are therefore made 2 % larger than the casting needs to be.
- Solidification shrinkage
- Cast a litre of molten metal, then lower the solidified piece into a full beaker of water, and it displaces only 9 dl. It has shrunk by 10 %. Put differently, the casting has increased its density.
GATING AND FEEDING
- Shrinkage cavity
- This defect, for example B200, appears when the feeding has not worked as intended, or when the need for feeding was missed altogether.
- Feeder
- A necessary evil that keeps shrinkage porosity out of the casting. Always placed on the thickest sections, and its modulus and volume must be greater than the section it feeds.
- Sprue
- The first part of the gating system. A vertical channel.
- Runner
- The second part of the gating system. It carries the metal onwards horizontally.
- Ingate
- The last part of the gating system. It leads the metal into the mould. A filter usually sits just before the ingate ends, to give laminar flow and to help keep the gating system full. You do not want to carry a lot of air down with the metal.
MOULD MAKING
- Location
- Keeps the mould halves correctly positioned in x and y, and helps you aim when closing the mould, so the cope is not set down on a core that could break.
- Coating
- A thin protective layer of zircon sand applied to mould and core before they are assembled into a finished mould. The coating has to be dry before assembly.
- Pattern board
- A flat board on which the pattern is mounted. There is also a gassing board version, for small moulds in longer runs.
- Core box
- Used to produce a core, which is one part of the mould. The metal solidifies against the core and forms the inside of the casting.
- Pattern
- Used to produce the cope and drag. The metal solidifies against that sand mould half and forms the outside of the casting.
- Moulding box
- A metal box set on the pattern board. It carries the pins and lugs that force the cope and drag together.
SAND TYPES
- Silica sand
- This covers both backing sand and facing sand. The names say what they are used for.
- Chromite sand
- If the facing sand cannot take the heat on heavier castings and starts to fuse with the metal, this is the alternative.
- Zircon sand
- The same again, and a last, even more expensive resort.
DEFECTS
- Crack
- There are both hot tears (C221) and cold cracks (C211). Hot tears form before the casting has fully solidified, because the sand does not yield once contraction has begun. Cold cracks form after the casting has solidified. Temperature has little to do with it, beyond the fact that hot tears form above the solidus temperature and cold cracks below it, at around 1400 °C. Not that cold, in other words.
- Gas porosity
- For example B111. There are many different causes and appearances: air, slag that forms gas, damp coating, binders, core gases and so on.
- Pore
- Let us slow down here. Which type are we talking about? There are several types, and even more causes.
HEAT TREATMENT
- Normalising
- Gives a uniform, fine-grained structure. Around 800 to 900 °C, cooled in air.
- Hardening
- The steel is heated to around 1 000 °C, up to a temperature where it is austenitic. When it is then quenched in water, the carbon atoms are forced into solution in a way that gives what is called a martensitic structure.
- Tempering
- A high temperature, within the range 400 to 700 °C, gives a soft material. A low temperature in the same range gives a harder one. Hardness can also be controlled through time at temperature. A long time gives a soft material, and the other way round.
- Quench and temper
- First a hardening, which leaves the steel hard and brittle, then a tempering, which makes it somewhat tougher and softer.
- Quenching
- After heat treatment of stainless, high-alloy steels, the temperature is brought down quickly from around 1100 °C to room temperature. The castings are quenched in water. This evens out differences in the material during the time at temperature, and the rapid quench avoids harmful phases forming at certain critical temperatures. A classic example is sigma phase in duplex steels.
- Slow cooling
- If there is no hurry, or if quenching is ruled out by the risk of distortion and cracking, the castings can be left to cool slowly after heat treatment.
OTHER
- Ladle
- The vessel used to carry the melt from the furnace to the mould for pouring.
Ready for the next step?
Get in touch and we will prepare a quote.