Steel foundry in Klavreström, Sweden. Stainless and acid-proof castings, from pattern to certified delivery.
Yes, we cast that.
GX5CrNiMo19-11-2 · 1.4408 to EN 10283/10213
Austenitic CrNiMo, acid-proof
Customers
Our castings sit inside pumps, valves, paper machines and vessels built by Sulzer, Alfa Laval, Xylem, Valmet, Somas, Stafsjö, Cellwood, Humphree, Log Max, Olvondo, Silver Weibull, Turab and FFS.
What they share is high demands on surface finish and pressure tightness.
55 designations in 31 production groups
Stainless and acid-proof is our speciality. Alloys in the same group share a composition window, so an EN grade and its ASTM equivalent are poured from the same melt. Pick a designation to look it up.
Austenitic stainless
1 group
Austenitic CrNiMo, acid-proof
4 groups
Superaustenitics
6 groups
Duplex and superduplex
8 groups
Martensitic
2 groups
Precipitation hardening
2 groups
Carbon steel and 13Cr
3 groups
White iron, high-chromium and manganese steel
5 groups
Can't find your grade? To order, we cast most common steel grades.
The full alloy programmeFrom sand mould to inspected casting
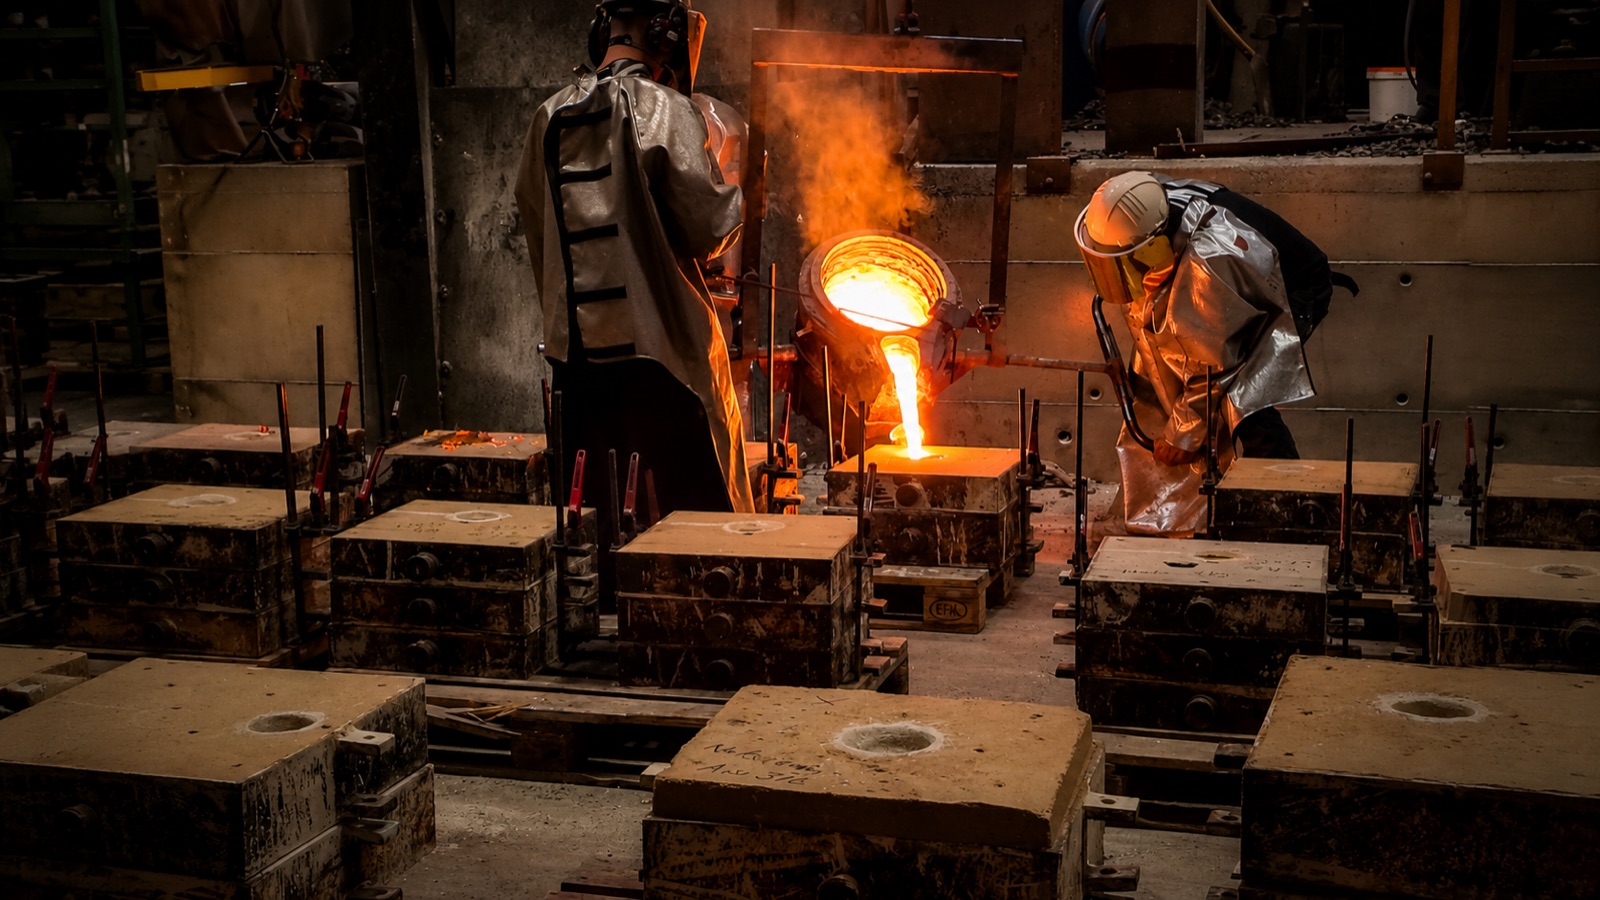
We cast by gravity in single-use sand moulds. Every part gets a new mould, which is broken apart to release the casting. Everything happens on one site, which is why lead times stay short.
-
Moulding the CO₂ method
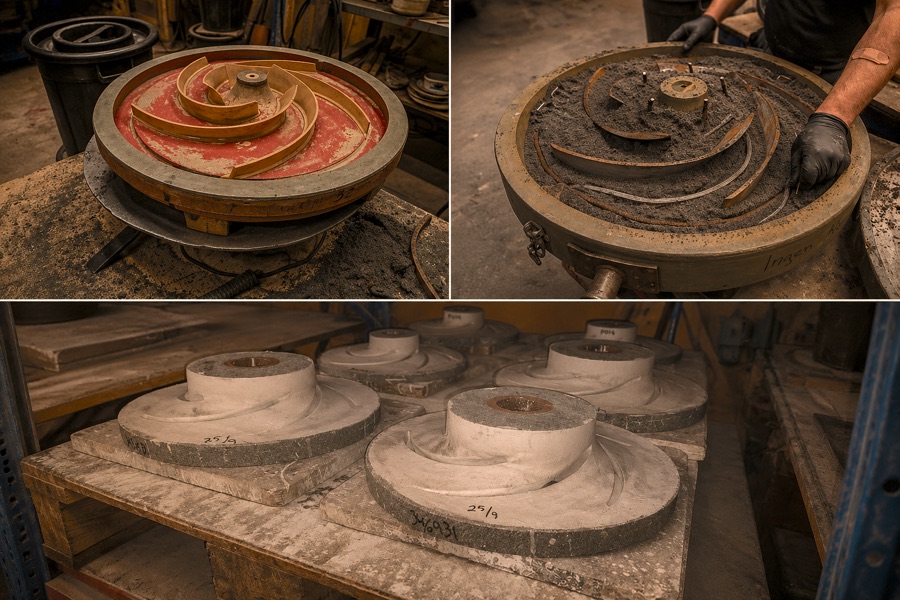
Pattern and core box. The pattern forms the outside of the casting, the core its inside. +2 %How much larger the pattern is made. The casting contracts as it cools.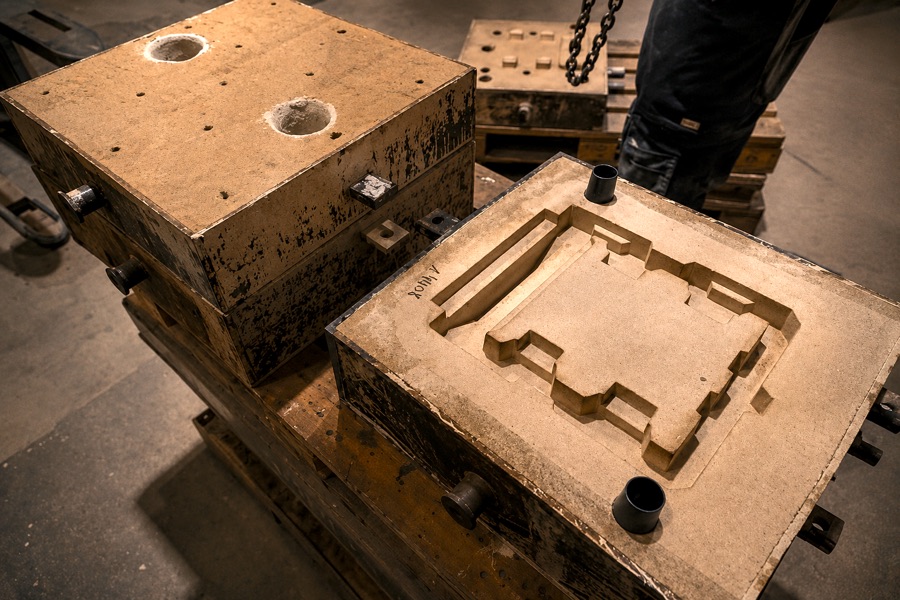
New sand, with zircon sand next to the pattern, gives fine surfaces and good dimensional accuracy. 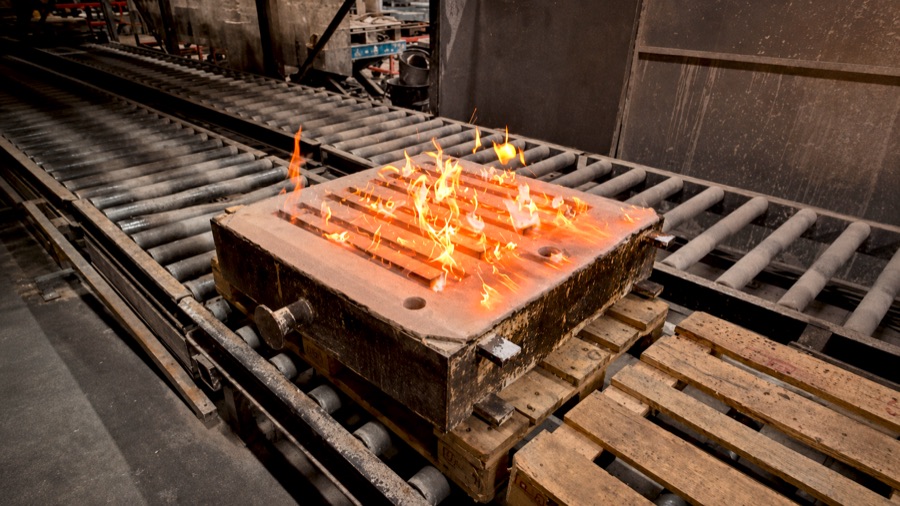
The spirit in the coating is burned off, leaving a protective layer. 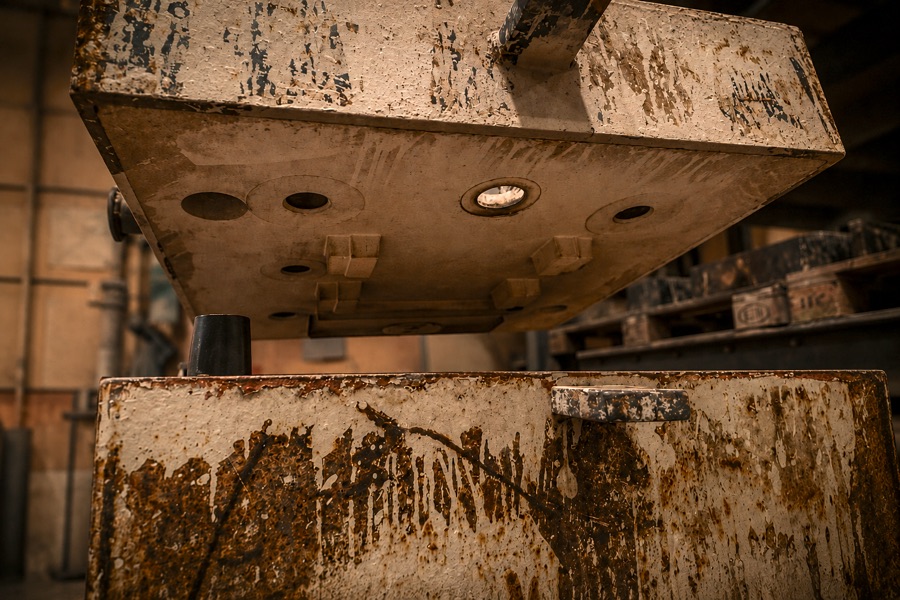
Mould halves and cores are assembled. -
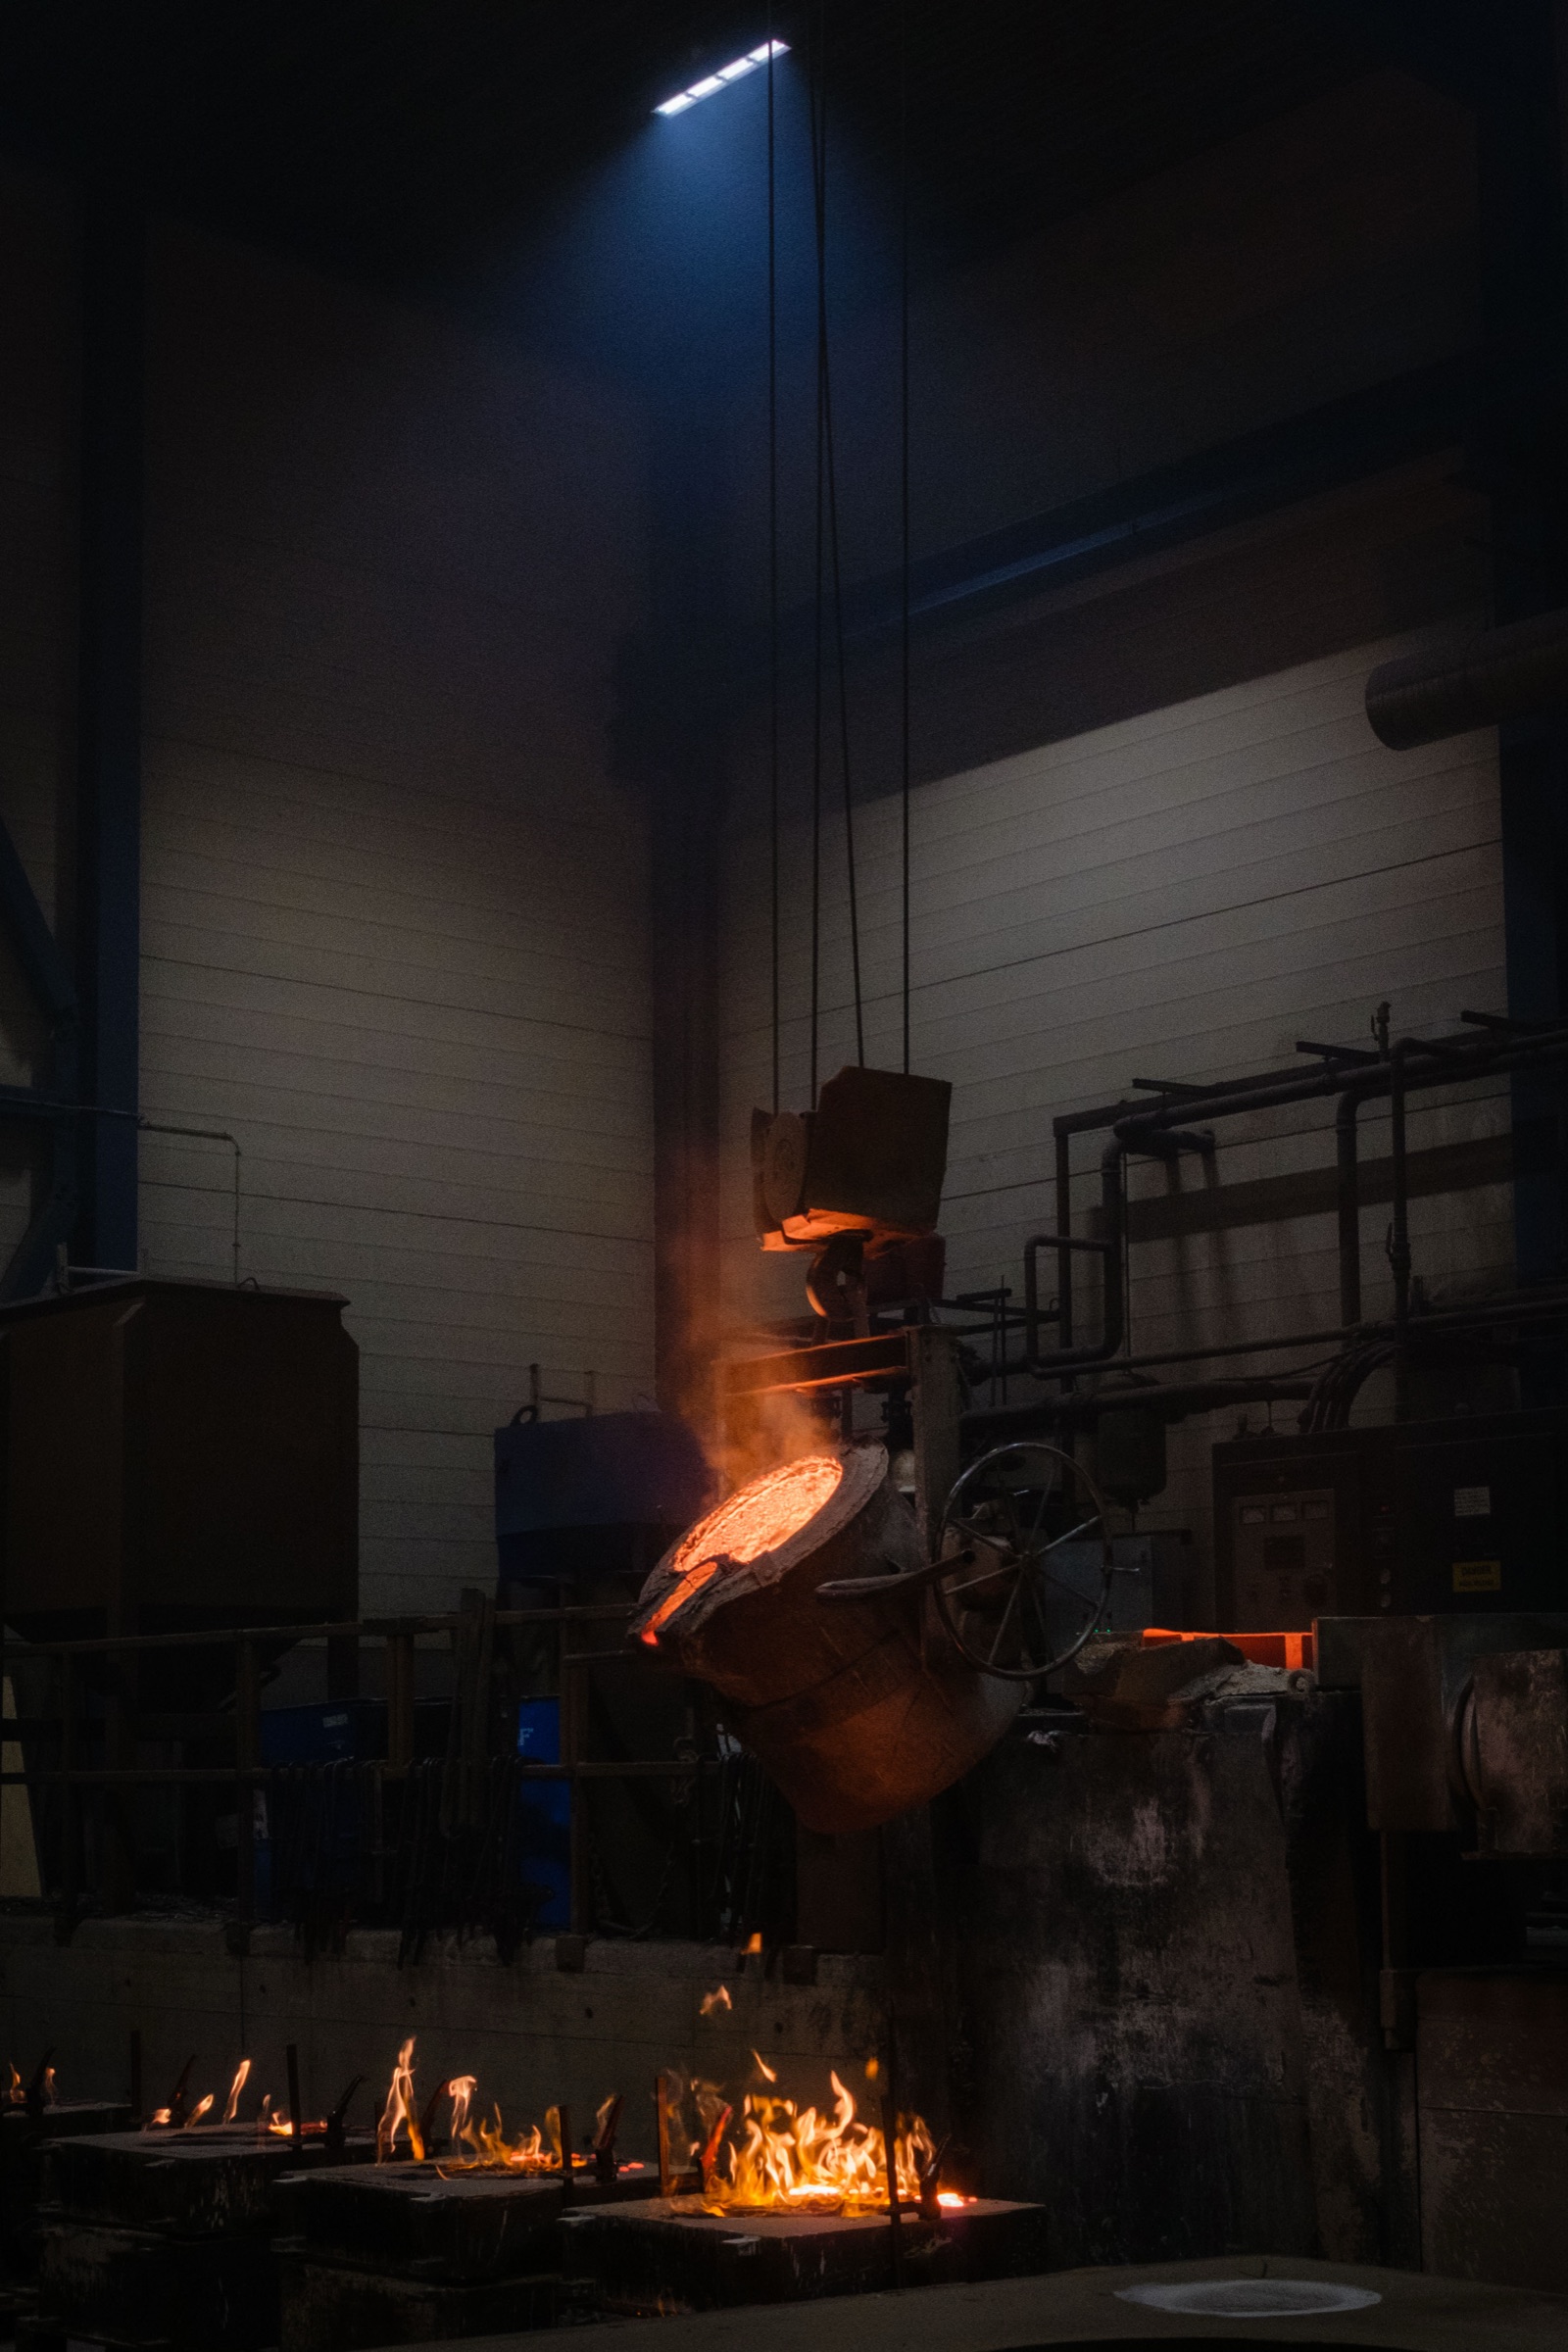
Casting low and full, without air or slag
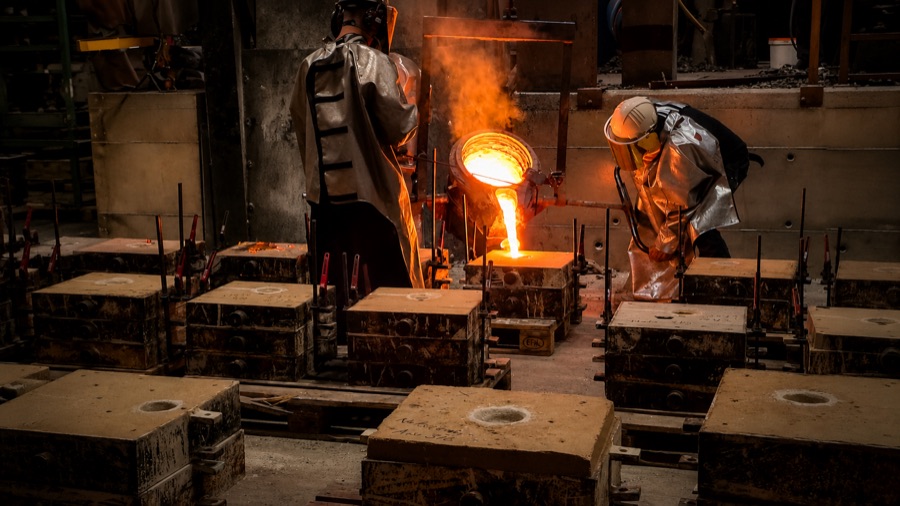
Pouring. The gating system keeps the flow calm all the way into the mould. 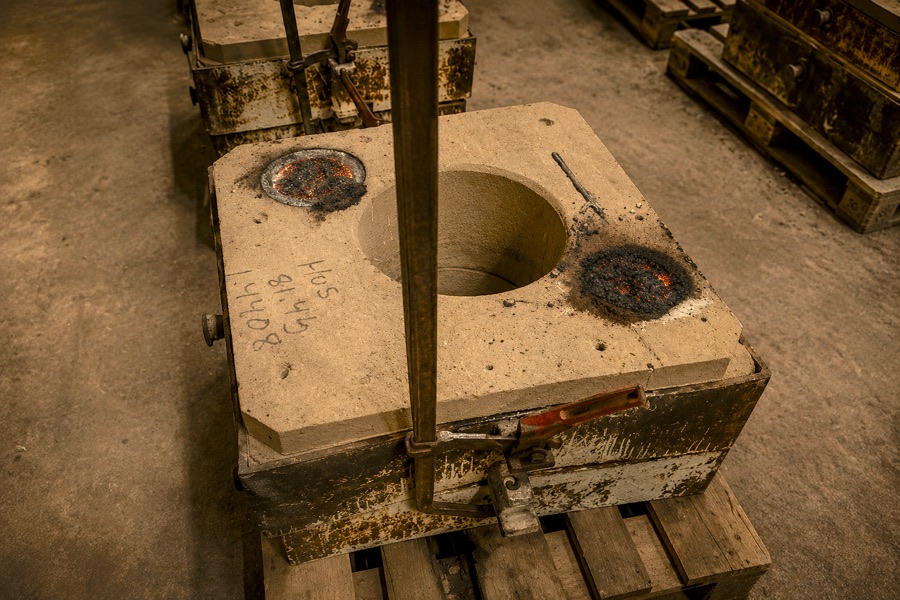
A poured mould. The alloy number is written in the sand. −10 %How much the steel shrinks as it solidifies. The feeders top it up meanwhile.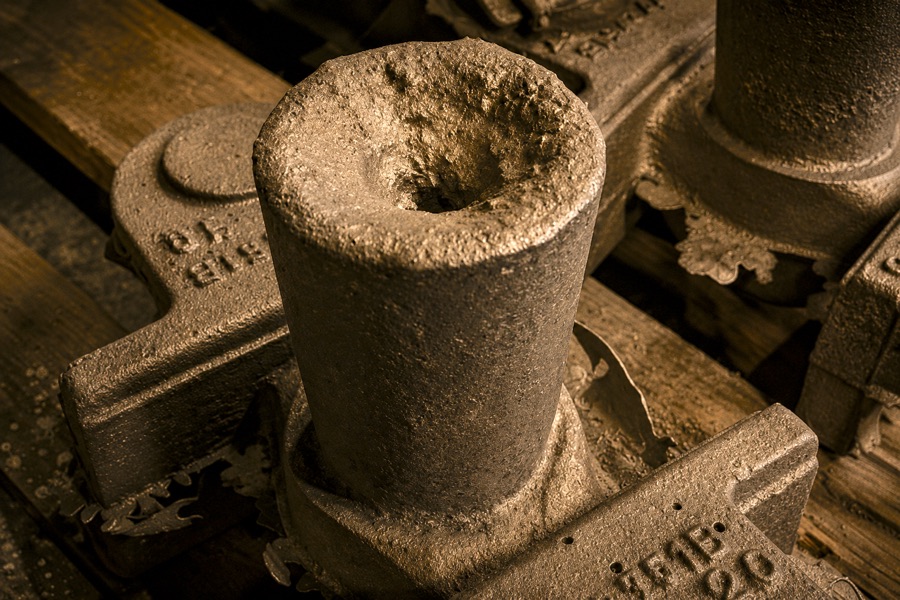
The shrinkage shows in the feeder, not in the casting. -
Finishing fettling, heat treatment, blasting
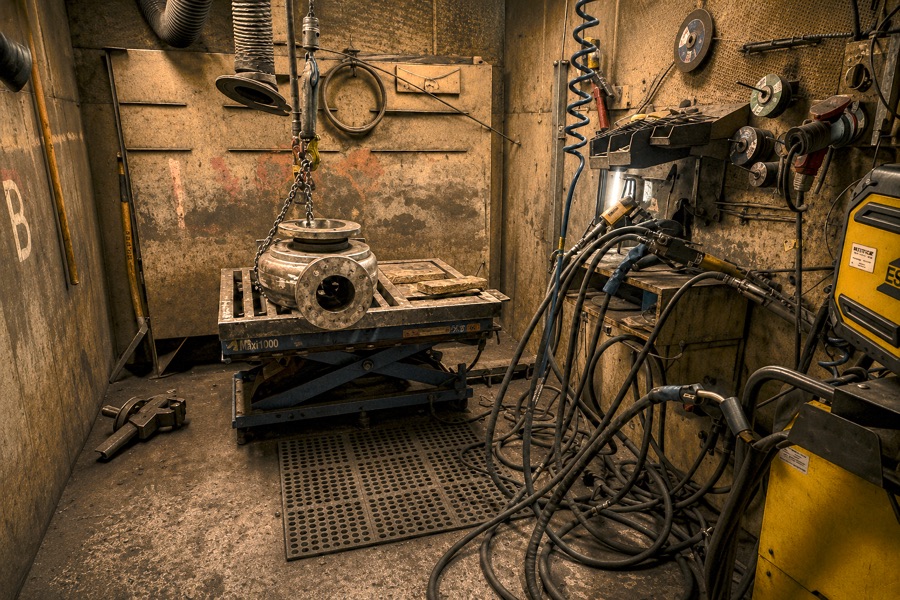
Fettling booth. Gating system and feeders are cut away, the casting is deburred. 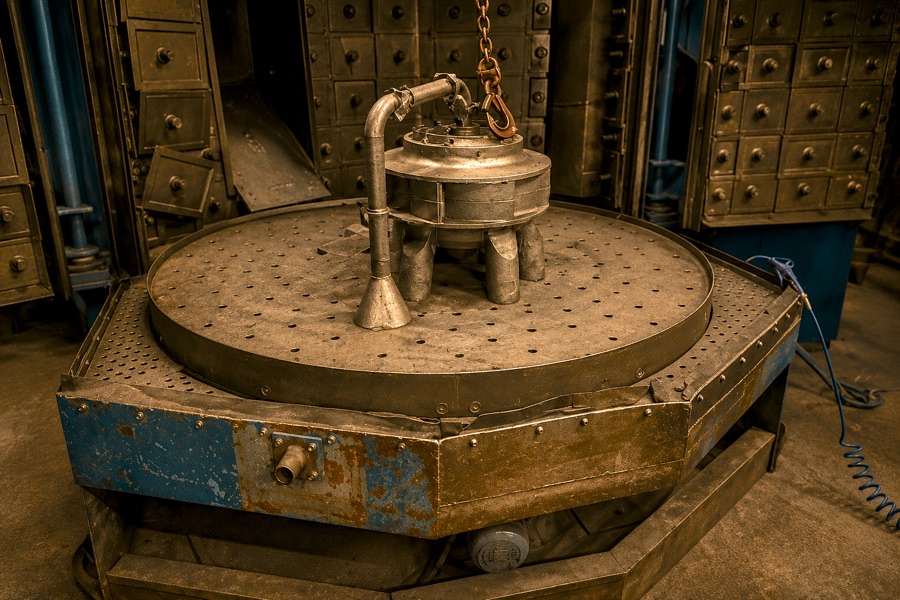
Blasting with a stainless medium removes scale before delivery.
The foundry in brief
- Method
- Gravity casting in single-use sand moulds. Moulds are made by the CO₂ method.
- Materials
- Stainless and acid-proof steel. Also duplex, martensitic, carbon steel, white iron and manganese steel.
- Heat treatment
- Our own furnace, fitted with a recorder. Every cycle can be followed and verified afterwards.
- Delivery
- As-cast blank or fully machined part, blasted with a stainless medium.
- Certificates
- ISO 9001:2015PDF, TÜV to PEDPDF, Bureau Veritas Mode II
- Policy
- Quality policyPDF, Environmental policyPDF
- Company
- Formed in 1998 through the merger of Klarviks Stålgjuteri and Klafreströms Stål. Part of Opima.